

-

Military Industrial Epoxy Floor System - Large Format 1500 SF & Larger
Military grade durability engineered for heavy duty service with a superior high gloss finish 12 Standard Colors
 Geared For Larger Projects - Sold By The SF to Match The Size Of Your Floor
 Turnkey Package To Do The Job Right
-

Industrial Grade Textured Non Slip Epoxy Coating
OSHA & ADA approved for concrete, steel and wood surface applications.
4 Colors Including Safety Yellow
Roll or Squeegee On For More or Less Aggressive Finish
Outperforms Retail Grade Nonslip Paints
-

Heavy Tonnage Industrial Epoxy Floor Coating
Toughest, longest lasting epoxy coating you can apply to any floor.
6 Standard Colors
2 Layers - Primer + Topcoat Epoxy
Bunker Hardened Finish
-

Industrial Epoxy Wall Coating
Best vertical wall epoxy coating for protection against abrasion and caustic washdowns.
7 Colors. Custom Colors Available
Fills In Cinder Block Voids In 1 Coat
DIY Friendly & Far Superior Than Paint!
-

Heavy Duty AG Epoxy Acid Shield
High performance Novolac System outperforms any type of standard floor epoxy
4 Colors - High Gloss Finish
2 Layers - Primer + Hardened Epoxy Topcoat
DIY Friendly - Save 80%
-

Self Leveling Urethane Epoxy Cement
When you need more than just a coating. This urethane cement is DIY easy and indestructible.
1/8-1/4" Thick
USDA & Health Department Approved
41 SF @ 1/8" Thick/Kit
-
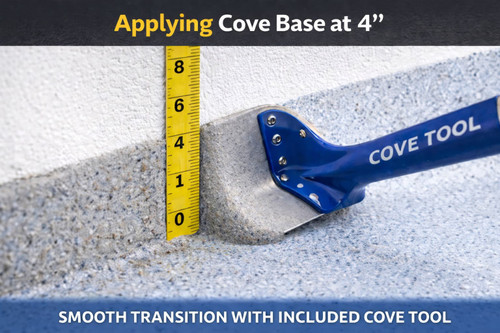
Cove Base Epoxy Kit
Epoxy liquids, aggregate and cove tool included. No prior experience required. Professional results!
Forms Seamless Transition From Floor To Wall
Eliminates Dirt & Bacteria Accumulation
Creates Waterproof Tub For Heavy Washdowns
Food & Beverage Facilities
Food & Beverage Processing Epoxy Floor Coatings
USDA-compliant, food-safe epoxy flooring systems engineered for production floors, breweries, commercial kitchens, bottling lines, and cold storage — built to withstand heavy forklift traffic, thermal shock, and daily caustic washdowns.
★ Food Safe • Free Shipping • Full Project Support✓Production Floor Epoxy & Urethane Cement Systems
✓Chemical & Acid Resistant Epoxy Flooring
✓Industrial Textured Non-Slip & Fast-Dry Options
✓Direct-to-Metal Equipment & Pipe Coatings
Three Epoxy Flooring Options For Food & Beverage Production Floors
Food and beverage facility floors face some of the most punishing conditions in any industry — constant forklift traffic, dropped tools and equipment, chemical spills, thermal shock from steam cleaning, and daily high-pressure caustic washdowns. Standard coatings fail within months under this kind of abuse.
Our Heavy Tonnage Epoxy System is engineered specifically for high-volume food production environments. This two-layer system features our high-performance primer — which outperforms most standalone epoxies — followed by a super-thick, chemically hardened topcoat that creates a surface several orders of magnitude harder than construction hard hats. It's the go-to system when you cannot afford floor failure or production downtime.
This system is food safe, waterproof, and withstands thousands of high-temperature caustic washdowns without losing its finish. It can be deployed across your entire facility worry-free — from production lines and packaging areas to loading docks and cold storage.
For heavy-duty processing areas, our Military Industrial System delivers exceptional durability at a lower price point. For medium-duty service areas such as break rooms, offices, and walkways, our Commercial Epoxy Flooring System provides a professional, long-lasting finish.

Ships free as a turnkey package — complete with everything needed for professional results. No prior application experience required.
Urethane Cement Epoxy Flooring
When building codes or facility specifications require a thicker floor installation, our Self-Leveling Urethane Cement is the solution. It can be applied up to 1/4" thick and is approved by health departments and building codes nationwide — making it the standard for USDA, FDA, and SQF-compliant processing facilities.
Urethane cement delivers what standard epoxy cannot: extreme impact resistance, thermal shock protection (critical for environments with steam cleaning and flash-freezing cycles), and a monolithic, seamless surface that eliminates bacteria harborage points. It's nontoxic and can be fully broadcast with sand or heavy aluminum oxide to provide a textured, non-slip finish.
Once broadcast, topcoat with either our commercial-grade two-part epoxy or our chemical and acid-resistant Novolac topcoat for environments that require protection against caustic washdown chemicals, CIP solutions, and food-grade sanitizers.
Easily applied with a cam/gauge rake and pin roller to release trapped air — no specialized equipment required.
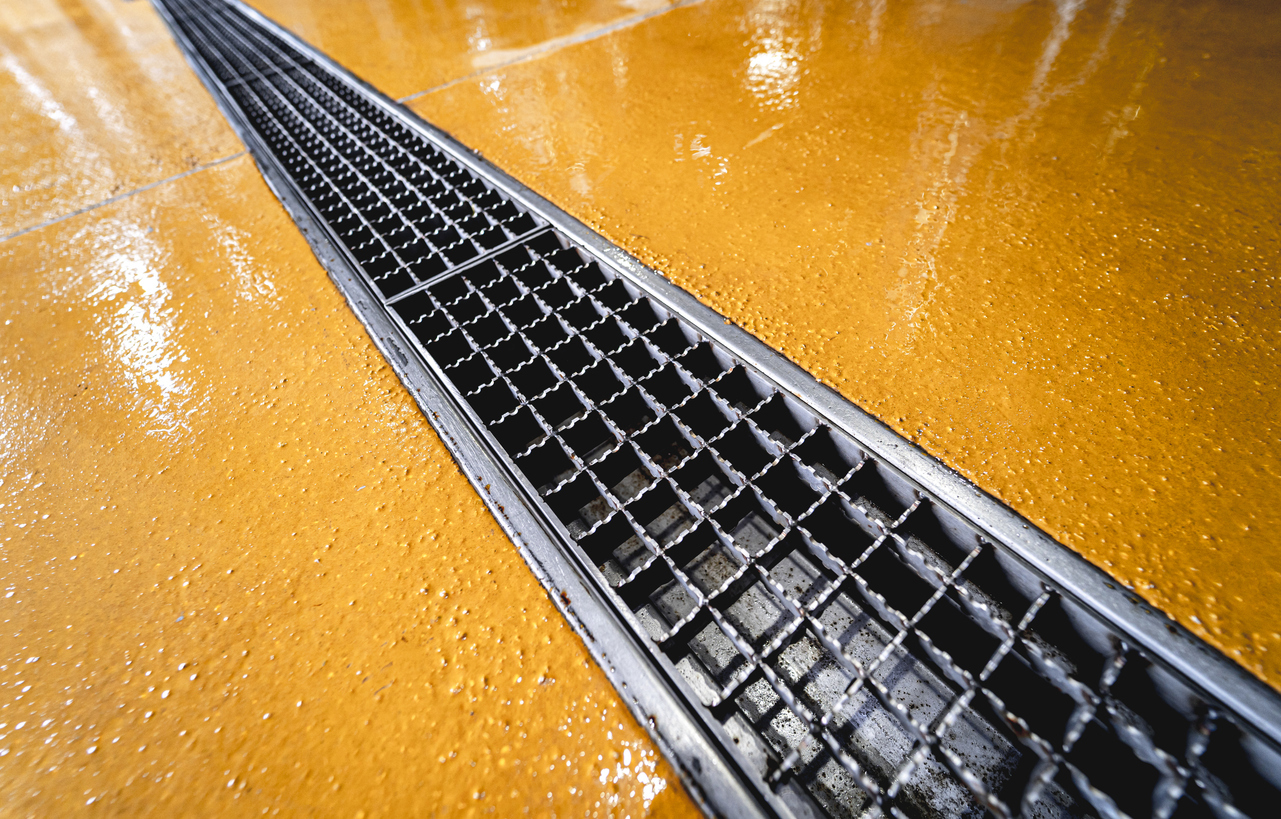
Image above: Close-up of urethane cement applied around a beverage production floor trench drain, fully broadcast and topcoated with commercial-grade epoxy in safety yellow.
Non-Slip Epoxy Flooring For Food Processing
Slip-and-fall incidents are among the leading causes of workplace injuries in food and beverage facilities. Wet production floors, grease, oils, and washdown water create constant slip hazards that standard smooth-finish coatings cannot address.
ArmorGarage offers two non-slip epoxy systems. Our Industrial Textured Non-Slip Coating features extra heavy duty epoxy infused with our proprietary blend of aggregates to create a textured durable surface with exceptional grip, even when wet or contaminated with oils and food byproducts. ArmorTrak is our flexible epoxy embedded with our proprietary dehydrated butyl rubber granules, unlike standard epoxies with low-grade rubber beads that quickly wear out of the coating. ArmorTrak is as tough as it is flexible and slip resistant.
Acid & Chemical Resistant Epoxy Flooring
Food and beverage production floors are subjected to aggressive chemical exposure on a daily basis — from CIP (clean-in-place) solutions and peracetic acid sanitizers to phosphoric acid, sodium hydroxide, citric acid, and dozens of other cleaning and processing chemicals.
Our Acid Shield systems are 100% Novolac epoxy — not a blend — engineered for sustained chemical exposure at both splash and immersion levels. They resist hundreds of chemicals and maintain their integrity through thousands of hot caustic washdown cycles, making them ideal for kill floors, bottling lines, dairy processing, brewery production areas, and any zone where chemical resistance is not optional.
Use our Acid Resistance Guide (300+ chemicals) to confirm suitability for your specific chemicals and exposure conditions before ordering.
Fast-Dry Epoxy Flooring Systems
Production downtime is money lost. In food and beverage facilities operating 24/7 or on tight turnaround schedules, floor coating projects need to be completed in the shortest possible window.
ArmorGarage fast-dry epoxy systems achieve walk-on cure in hours — not days — allowing you to return your production floor to full service the same day or overnight. These accelerated-cure formulations deliver the same chemical resistance, abrasion ratings, and food-safe compliance as our standard systems, with dramatically reduced downtime.
Ideal for scheduled shutdowns, weekend turnarounds, and phased installation in facilities that cannot take an entire production floor offline at once. Contact our team to discuss scheduling and fast-cure options for your project timeline.
Direct-to-Metal Epoxy Mastic For Equipment & Infrastructure
Your floor isn't the only surface that needs protection. ArmorGarage's direct-to-metal epoxy mastic is purpose-built for the piping, machinery, structural steel, equipment housings, and building infrastructure found in food and beverage processing facilities.
This is not a standard paint or thin-film primer. Our epoxy mastic applies super thick in a single coat, building up to create a seamless, protective barrier that bridges surface imperfections and rounds out sharp corners and weld seams — eliminating the corrosion-prone edges and crevices where moisture and chemicals attack first. The result is a smooth, monolithic coating that is dramatically easier to clean and inspect.
Applies directly to steel with minimal surface preparation — no sandblasting to white metal required. Ideal for process piping, tank exteriors, structural columns, conveyor frames, equipment supports, mezzanine steel, and overhead infrastructure. Also available for wall and ceiling applications.
One-stop facility coverage: From production floors and trench drains to overhead piping, equipment, roofing, and even leaky cooling towers — ArmorGarage has a coating engineered for every surface in your food and beverage facility.
Food & Beverage Production Floors — Questions We Get Asked Most
Straight answers based on our experience both as a manufacturer and at one time one of largest installers in the NY Tri_Stae area on coating plant floors, walls and equipment.
What is the best epoxy floor for a food production plant?
+
For high-volume production floors our first choice is the Heavy Tonnage Epoxy System. It is a two-layer system — a high-performance primer that outperforms most standalone epoxies, followed by a super-thick, chemically hardened topcoat — and it's the one we spec when floor failure or downtime is simply not an option. It's food safe, waterproof, and holds its finish through thousands of hot caustic washdowns and constant heavy forklift traffic.
For heavy-duty processing areas that don't see that level of abuse, our Military Industrial System delivers the durability at a lower price point. For break rooms, offices and walkways, our Commercial Epoxy Flooring System is the right fit. All three ship free as complete turnkey packages.
When do I need urethane cement instead of an epoxy coating?
+
Three situations. First, when your building code, facility spec or SQF program calls for a thicker floor than a coating can provide — our Self-Leveling Urethane Cement goes on up to 1/4" thick and is approved by health departments and building codes nationwide. Second, when the floor sees thermal shock: steam cleaning, hot washdowns and flash-freezing cycles will eventually crack a rigid epoxy, while urethane cement is built to move with the slab. Third, when the concrete is beat up and you need a new wearing surface rather than a coating over damaged concrete.
It's applied with a cam/gauge rake and pin roller, broadcast with sand or aluminum oxide for texture, and topcoated with our commercial epoxy or the Novolac Acid Shield topcoat. No specialized equipment required.
Is epoxy flooring USDA and FDA approved for food and beverage facilities?
+
Yes. Our food and beverage floor systems are USDA compliant and food safe, and our urethane cement is the standard for USDA, FDA and SQF-compliant processing facilities. What inspectors are checking for is a floor that is seamless, non-porous, chemical resistant and cleanable with no cracks or joints for bacteria to harbor in. A properly installed epoxy or urethane cement floor meets that; bare, painted or tiled concrete does not. Finish the wall joint with our epoxy cove base and the whole floor becomes one washable, monolithic surface.
Will epoxy hold up to forklift traffic and dropped equipment?
+
Industrial-grade epoxy will; retail garage or water-based epoxies will not. The difference is film thickness and hardness. Thin coatings get cut by forklift tires turning under load and chip where tools and parts land. Our Heavy Tonnage System is engineered for exactly that — the primer locks into the concrete and the thick, chemically hardened topcoat takes the impact and abrasion instead of the slab, curing to a surface several orders of magnitude harder than a construction hard hat.
If the floor also takes frequent heavy impacs from steel-wheeled carts, dropped totes or heavy falling objects, step up to urethane cement for extreme impact resistance.
Which floor coating stands up to CIP chemicals and sanitizers?
+
A true Novolac epoxy. Our Acid Shield systems are 100% Novolac — not a blend — and are built for sustained exposure at both splash and immersion levels to peracetic acid, phosphoric acid, sodium hydroxide, citric acid and the rest of the CIP and sanitizer lineup. They hold their integrity through thousands of hot caustic washdown cycles, which is why we spec them for kill floors, bottling lines, dairy processing and brewery production areas.
Before you order, check your specific chemicals and concentrations against our Acid Resistance Guide, which covers over 300 chemicals. If you're washing down with something unusual, send us the SDS and we'll confirm.
How do we recoat the floor without shutting down production?
+
Two ways. Our fast-dry epoxy systems reach walk-on cure in hours rather than days, so a floor coated on a scheduled shutdown or over a weekend is back in service the same day or overnight. They carry the same chemical resistance, abrasion rating and food-safe compliance as our standard systems — only the cure schedule is accelerated.
For plants that can't take a whole floor offline at once, we plan a phased installation: coat one zone per turnaround while the rest of the line keeps running. Tell us your shutdown windows and we'll build the schedule around them.
Which non-slip epoxy is right for a food processing floor?
+
It depends on whether you need maximum grip or flexibility. Our Industrial Textured Non-Slip Coating is extra heavy duty epoxy loaded with our proprietary micro aggregate blend — the highest traction level we offer, and it keeps its grip when the floor is wet or contaminated with oils and food byproducts. Choose it for washdown zones, dock areas and anywhere workers move quickly with loads.
ArmorTrak is our flexible epoxy embedded with dehydrated butyl rubber granules — unlike the low-grade rubber beads in standard rubberized coatings, ours don't wear out of the film. Choose it for floors that flex, see thermal movement, or where you want traction with a slightly softer feel underfoot.
Both the Heavy Tonnage System and the Urethane Cement System can use several types of nonslip additives in theor topcoats for maximum traction.
Can our own maintenance crew install it, or do we need a contractor?
+
Your crew can install every system on this page. The epoxy systems are roller-applied and ship as turnkey packages with everything needed — no prior coating experience required. Urethane cement is applied with a cam/gauge rake and pin roller, both standard tools. Our coating experts support your crew seven days a week before, during and after the job. If you'd rather use a contractor, we'll supply the materials and support them directly.
What do you use on piping, tanks and structural steel in a food plant?
+
Our direct-to-metal epoxy mastic. It is not a thin-film paint or primer — it applies super thick in a single coat and rounds out sharp corners and weld seams, which are exactly where corrosion starts. The result is a smooth, very durable monolithic surface that is easier to clean and inspect on process piping, tank exteriors, structural columns, conveyor frames, equipment supports and overhead steel.
It goes on with minimal prep and no sandblasting to white metal, and the same product is available for walls and ceilings — so you can coat every surface in the plant from one supplier with one support line.
Ready to get started? See individual product pages for specifications, coverage rates, and installation details. For project pricing, volume discounts, or help selecting the right system, call 866-532-3979 or Request a Quote.